DETSCH 63 DASH pipe bending machine

Introduction to outstanding performance characteristics

Introduction to Machine Performance Features
1.The machine head and the three-way bed are welded from high-strength Q345 or 16Mn steel plates, with a design of staggered reinforcing ribs, annealed to eliminate internal stress, and shot blasted. The bed has sufficient strength and rigidity, with no vibration during core bending, preventing permanent deformation. Simultaneously, it provides a high-precision foundation for three 90° distributed heavy-duty roller linear tracks. The entire machine is processed by a gantry machining center, ensuring extremely high precision for the bed and machine head (utility model patent).
2.The main spindle and bending chain wheels are integrally forged with 42CrMo alloy steel, processed integrally, with integral hobbing, no key connection, and quenched and tempered, as well as locally high-frequency quenched and ground (utility model patent). The actual load of the chain is 36% of the rated load, with a design service life of 30 years.
3.The bending drive structure generates torque through double oil cylinder pulling the bending chain wheels. The large rod diameter structure of the bending oil cylinder, with a cylinder diameter to rod diameter ratio of 2:1, has great bending resistance. The threaded connection of the rod diameter inside the chain ensures smooth and reliable transmission without pulsation (utility model patent). The return reset cylinder also has the advantages of a large rod diameter and provides rapid reset function. The return reset speed is 1.79 times the bending speed, greatly improving work efficiency.
4.The transmission spindle system is equipped with two German FAG self-aligning roller bearings, directly heat-mounted from the upper part of the machine head, with extremely high assembly accuracy. During bending, the main spindle can simultaneously bear large radial and axial combined loads, with almost zero radial and axial jump, good precision retention, and easy and quick disassembly and maintenance. It forms a sophisticated and durable three-layer shaft system structure with the main die reset and mold opening and closing functional modules (invention patent).
5.Mold opening and closing functional module: The demolding mechanism is a three-linkage self-locking mechanism. During bending, the main die closes and locks as a whole. After bending, the main die opens, greatly solving the difficulty of unloading materials for square pipes, angle steels, flat steels, and asymmetric profiles (especially for bending angles ≥180°), making it convenient for refeeding and clamping (invention patent).
6.The clamping and pressing actions adopt an extremely stable and reliable three-linkage amplification self-locking structure. The flat-pushing clamping and pressing avoid the displacement of the pipe material during clamping, as seen in the sinking-type clamping structure! The clamping assembly and pressing assembly (including auxiliary pushing) have aluminum bronze (QATG-A, embedded graphite) inlaid on their active surfaces (straight sliding surface or curved surface) and are automatically lubricated at regular intervals.
7.The auxiliary pushing cylinder is installed in the auxiliary pushing frame (the top forging cylinder and top forging frame of the top forging module are integrally forged with 40Cr and quenched and tempered). Under the same stroke, the auxiliary pushing (top forging) mechanism effectively reduces the length of the auxiliary pushing (top forging) mechanism, avoiding the waste of straight segments of bent pipe parts due to the length of the auxiliary pushing (top forging) mechanism.
8.Material grabbing, corner turning, and feeding trolley are installed on the innovative three-way bed (not applicable to CNC type, NC type does not have this item):
8.1. The trolley material grabbing (cannon barrel) action is completed by the built-in hollow structure cylinder pushing the 15° elastic chuck, with a compact and extremely stable structure, strong clamping force, and no displacement of the pipe material during clamping (invention patent), ensuring extremely high clamping precision (the trolley does not slip during bending or top forging operations).
8.2. The trolley feeding is completed by the servo motor driving the precision planetary reducer gear (including the double gear rack backlash elimination module) to push the rack, with stable and reliable pushing structure (additional modules can convert the feeding pushing force into bending pushing force or top forging force to achieve: bending into large radius arc, whole circle, spring-like spiral pipe, or extreme small radius 1D top forging bending).
8.3. The trolley corner turning is completed by the servo motor driving the secondary enveloping worm gear and worm pair through the precision planetary reducer (not ordinary worm gear and worm), with large transmission torque, high transmission efficiency, small backlash and back clearance, high precision, long life, and the trolley can rotate while pushing bending to make helical coil.
9.The unique hollow double piston rod cylinder core pulling function module (special function module needs to be ordered separately, utility model patent):
9.1. Self-lubricating, during bending, oil can be forcefully injected into the inserted pipe through the hollow rod for automatic lubrication of the multi-ball core shaft inside, greatly improving the life of the core shaft and the quality of the bend.
9.2. Slow core pulling, while bending extremely small radius thin-walled pipes, the multi-ball core shaft at the bend is slowly pulled out, with excellent roundness correction and wrinkle removal.
9.3. The tail end piston rod stroke adjuster adjusts the position of the core rod inserted into the pipe fitting to achieve the best bending effect.
10.Independent external hydraulic pump station with condensation and heating functions, capable of continuous operation for 72 hours without interruption, also easy for maintenance and adding functional modules, with practical and reasonable design and extremely stable performance.
Main technical parameters
| Name | Value | Unit |
|---|---|---|
| Bending Spindle Diameter | Φ200 | mm |
| Rated Bending Torque | 52436.44 | N*M |
| Maximum Bending Torque | 97568.66 | N*M |
| Rated Pipe Bending Capacity | Φ63.5X10XR63.5 | mm*mm*mm |
| Bending Radius Range | 20-300 | mm |
| Bending Angle Range | 0-200 | ° |
| Swing Arm Bending Speed | 0-4 | r/min |
| Opening and Closing Mold Stroke | 90 | mm |
Our Pipe Bending Machine Customers
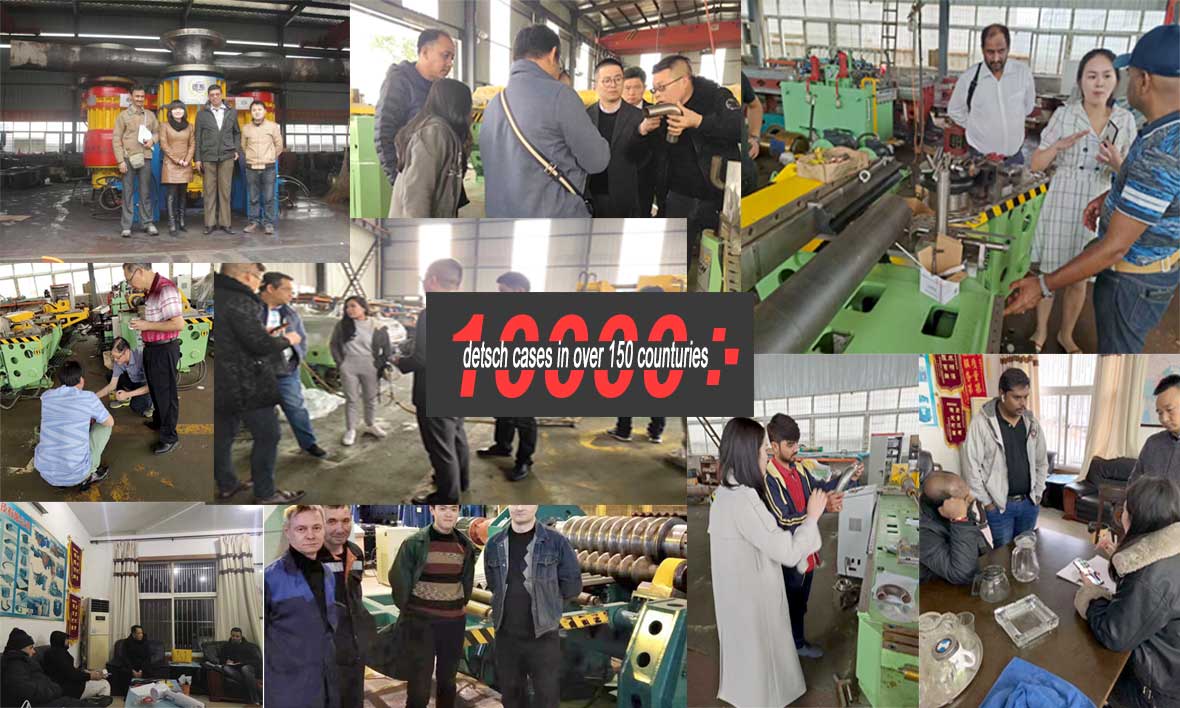
So far, we have sent our machines to more than 100 countries and regions, such as (Algeria, Argentina, Australia, Bangladesh, belarus, Bhutan, Bolivia, Brazil, Cambodia, Columbia, Congo, the Czech republic, Paraguay, Philippines, Qatar, Russia, Senegal, seychelles, Sri Lanka, Syria, Thailand, Trinidad and Tobago, Uganda, Ukraine, Ukraine, United Arab Emirates, USA, Uzbekistan, Vietnam, etc.)
If you are unable to visit our company during the pandemic, you can always contact us and check a 360-degree video of our factory workshop.
Warmly welcome you to visit us! We hope that the epidemic will end soon.
Best wishes